TTE, MSCED, TRD, CT

Aluminum Extrusion Press Tooling Up to 96” and 100,000 lbs.

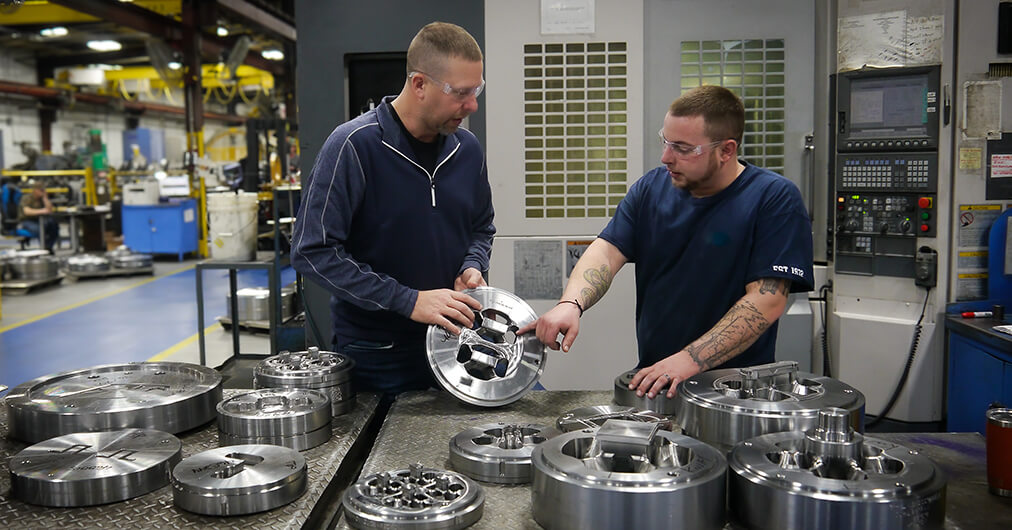
Our press tooling team builds tooling for 120+ extruders running 2 to 20 presses each. When your rep picks up the phone, you’re talking to someone who understands aluminum extrusion and the tools that keep the press running.

Press Tooling Customers
120 +
Up to 96" in Length & Diameter
96 "
Up to 100,000 LB. Weight Capacity
100000

Same-Business-Day

Same-Business-Day Emergency Response

Containers, Dummy Blocks, Stems, Shear Blades, and Die Cassettes

Up to 96” in length and diameter, up to 100,000 lbs.

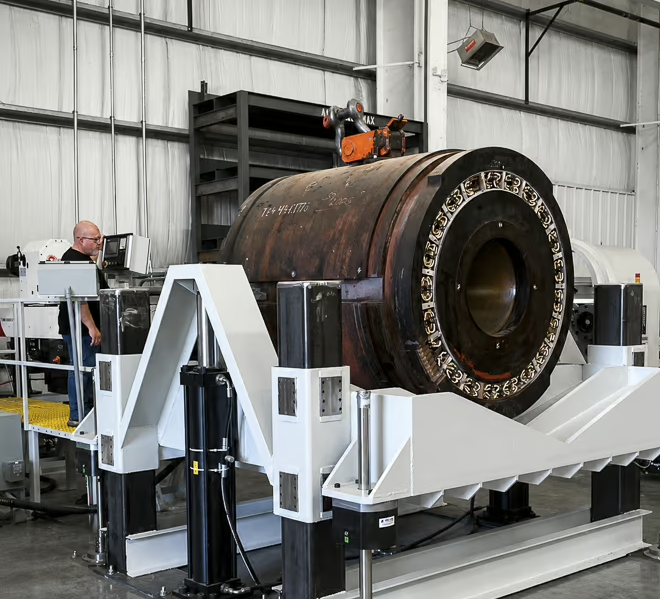
Aluminum extrusion container mounted on a reline fixture in the shop.

Product Range

  • Pressure rings and plates
  • Bolsters, bolster holders, and die rings
  • Die cassettes and horseshoes
  • Shear blades and butt knockers
  • Containers, liners/relines, and heating systems
  • Dummy blocks, including quick-change designs built for fast rotation
  • Stems and stem collars
  • Cleanout blocks, for both cold and hot applications
  • Alignment barrels and billet failers

We choose the steel, heat treat, and surface finish for each part and the press it runs in, so components hold their dimensions and stay in service longer.

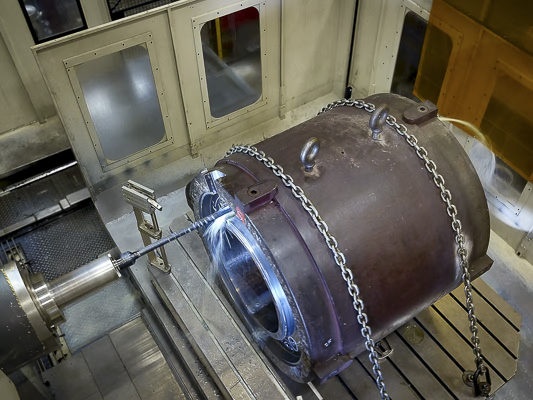
Extrusion container chained into a horizontal boring mill.
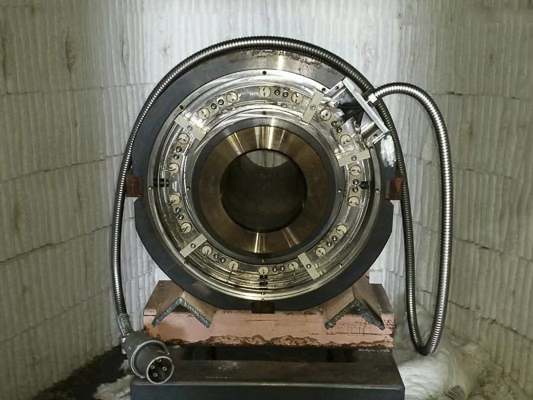
An aluminum extrusion container with exposed heating system elements.
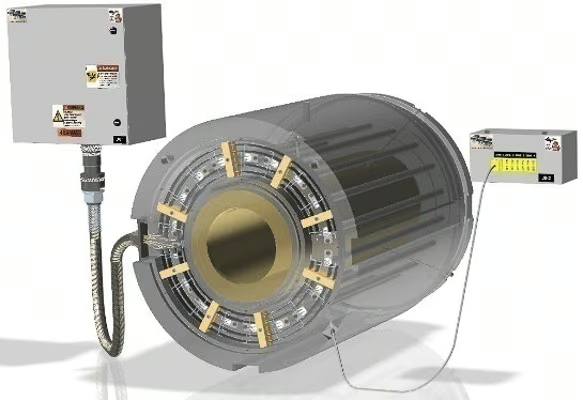
Cutaway rendering of an extrusion container with heating elements and control boxes.
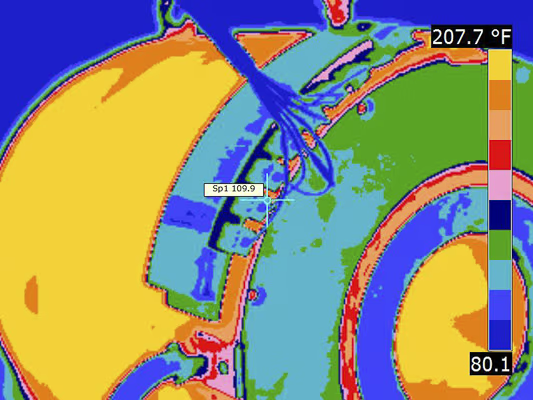
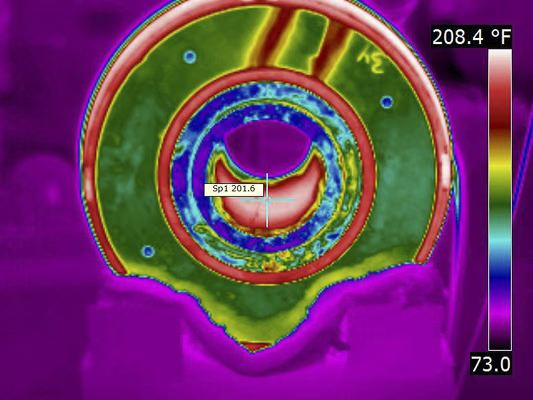
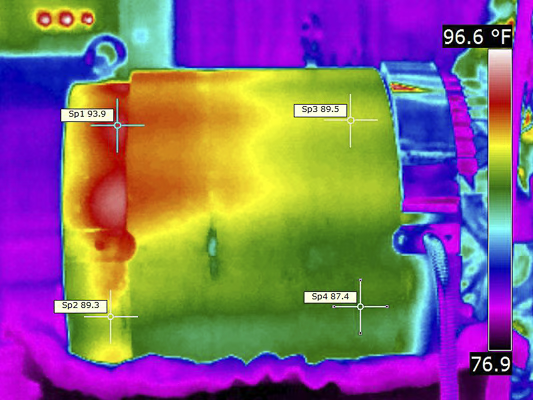
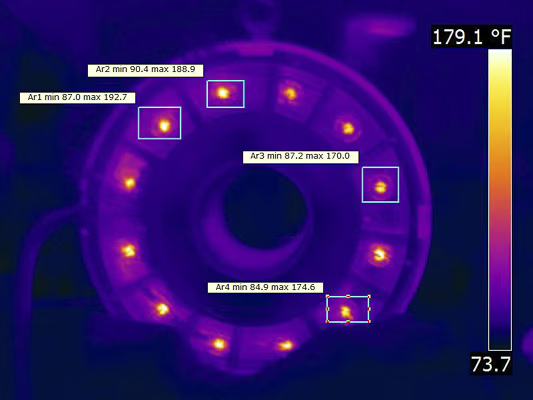
Thermal image of an extrusion container showing heat distribution across the liner.
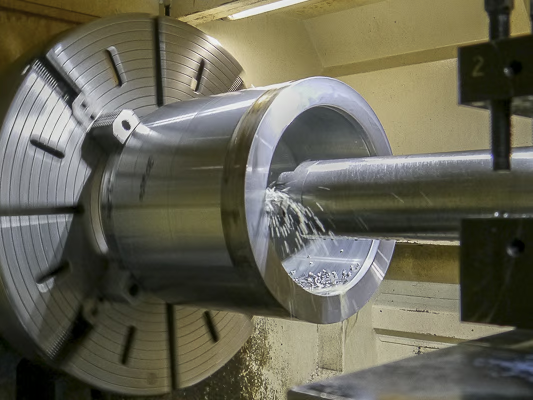
An extrusion container liner being machined on a horizontal boring lathe.
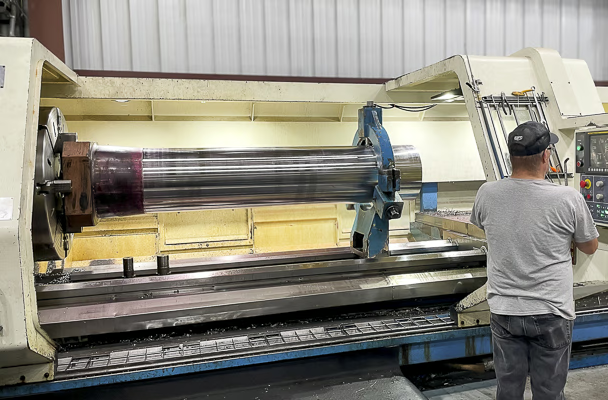
Operator machining an aluminum extrusion stem on a horizontal lathe.
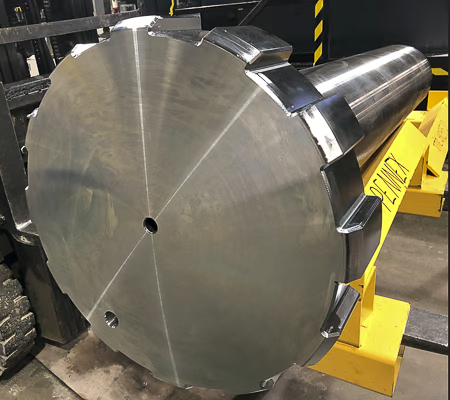
Extrusion press stem after being machined.
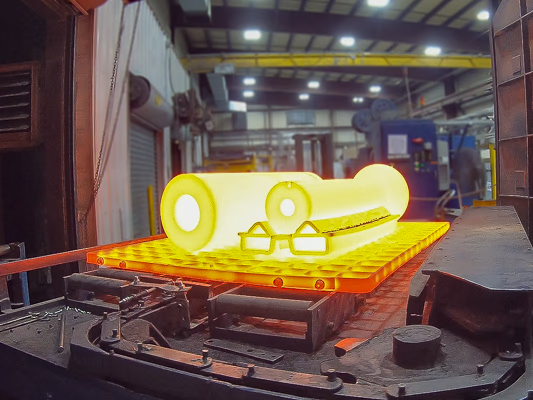
Extrusion stem and liner glowing on the transfer table after leaving a heat treat furnace.
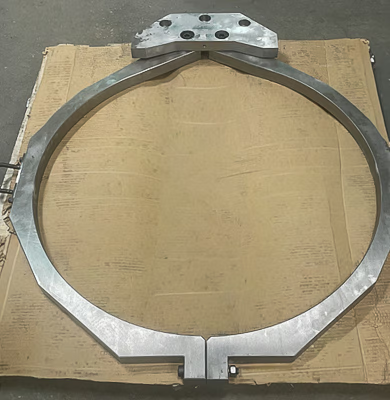
Container clamps, A.K.A “retainer rings,” laying on cardboard.
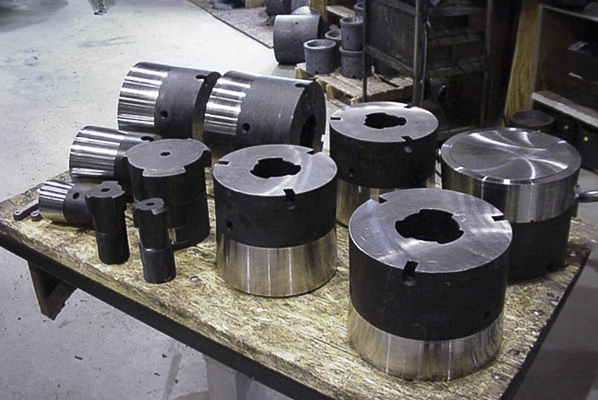
Set of fully assembled extrusion dummy blocks alongside individual dummy block components.
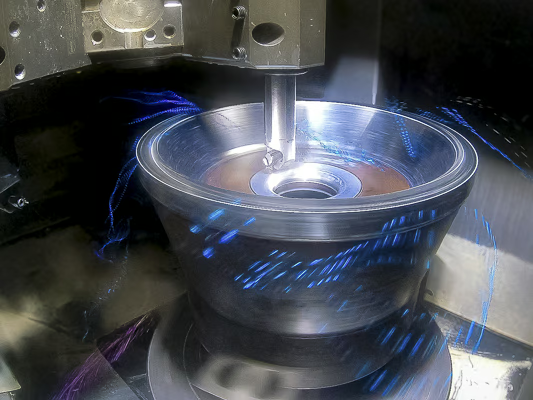
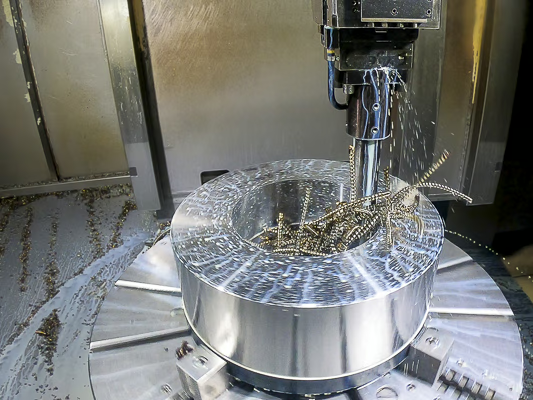
Dummy block being finished on a vertical lathe
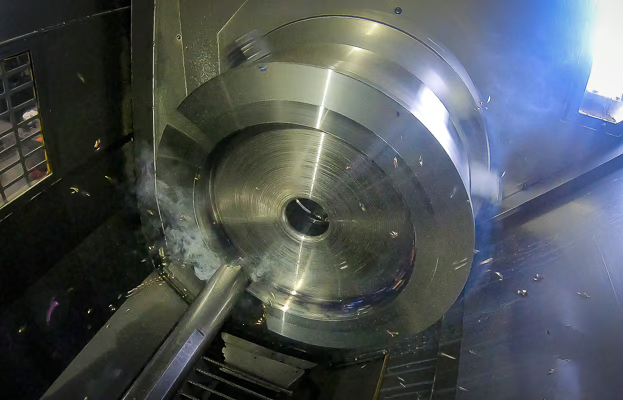
Dummy block being machined on a horizontal lathe.
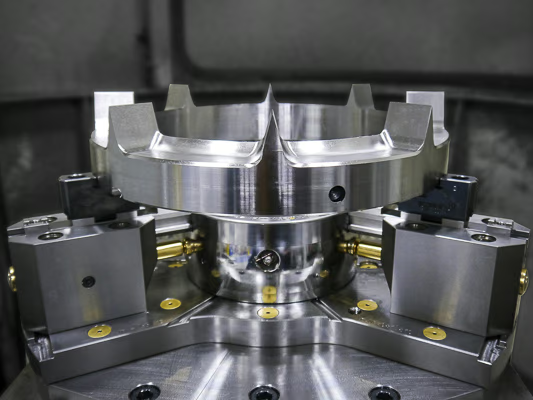
Extrusion die ring being bored on a vertical mill.
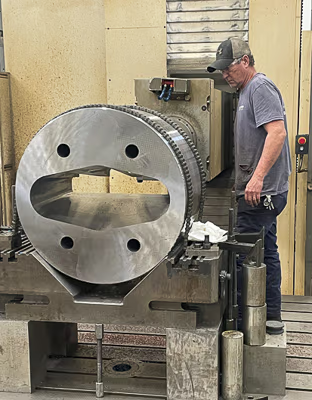
Machine operator standing next to a large extrusion bolster suspended on a horizontal CNC mill.
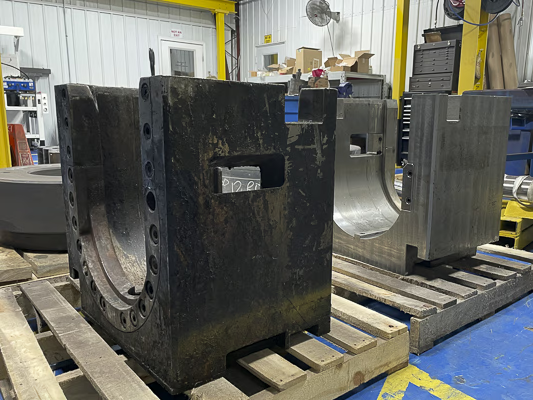
Two refurbished extrusion die cassettes, A.K.A “carriers” sitting on wooden pallets.
New extrusion die cassette sitting on wooden blocks.
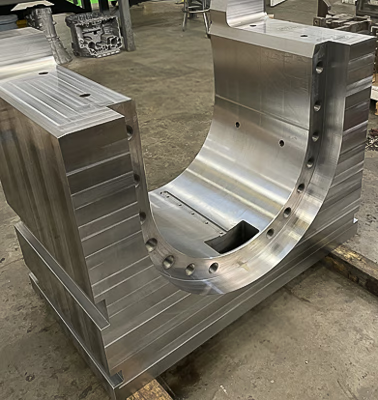
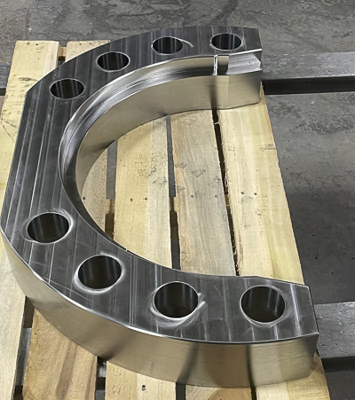
Machined horseshoe-shaped press tooling component with a bolt-hole pattern.
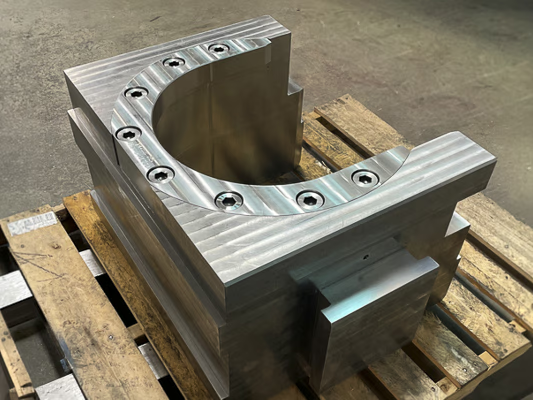
A horseshoe installed in an extrusion die cassette.
Extrusion scalper blade being machined in a CNC machine.
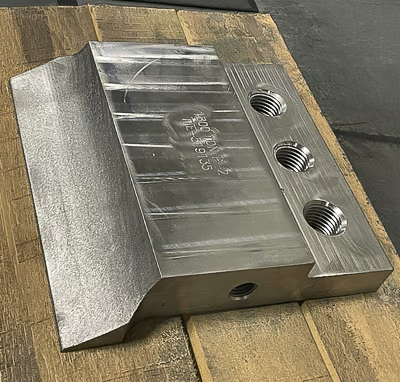
New extrusion shear blade on a wooden palette.

Container

Container getting holes machined for a heating system.

Capacity Snapshot

SpecificationValue
Maximum dimensions96" in length and diameter
Maximum weight100,000 lbs.
Press tooling customers120+
Presses per customer2 to 20
Emergency responseSame business day, never more than 24 hours

Support at the Press

Beyond building the tooling itself, our team supports you at the press:

  • On-site troubleshooting
  • Pre-press install preparation and planning
  • New press start-up support to resolve tooling and extrusion issues at launch
  • Preventive maintenance support
  • Overall equipment efficiency (OEE) improvements

Our press tooling design team works with 120+ customers, each running 2 to 20 presses. They’ve seen just about every press setup and can hold a real technical conversation about yours.

Plan Ahead: Dummy Block Stock and Container Relines

Most extruders we work with put unplanned downtime somewhere around $2,500 an hour. Dummy blocks and containers are the two most common culprits.

We can’t prevent every failure, but we can help you prepare for one.

Dummy Blocks

Running out of dummy blocks is the most common reason extruders call us for an emergency shipment. We stock dummy blocks for 90+ customers, including quick-change designs built for fast rotation, and we carry the inventory cost so you can spend that money keeping the press running.

Containers

Container liners wear slowly enough that operators often don’t notice until output is already slipping. A reline costs a fraction of a new container and can recover that lost output. We recommend keeping a backup container with a new or refurbished liner on hand. We run four container relines a week, and if your container has an on-board heating system, we’ll tune it up while it’s here.

Emergency Tooling Requests

Our press tooling team responds to every emergency tooling request the same business day, never more than 24 hours. With over 300 employees working around the clock and 155 mills, lathes, EDMs, and grinders, you have tooling in hand in days, not weeks.

Recent Emergency Turnarounds

Container reline: relined and delivered 3 days
3 Days
New container: built, delivered, and in the press 8 days
8 Days
Shear blade: delivered in 5 days to a new customer, no prior relationship
5 Days

Same-Day

Dummy blocks: custom configurations stocked for over 90 customers, shipped the same-day

Those aren’t a guarantee, but they’re real examples and they’re what we mean by “tool in hand in days, not weeks.”

Aluminum Extrusion Press Tooling FAQ

Press Tooling FAQs
+
-

What press tooling do you build for aluminum extrusion presses?

Containers and liners, dummy blocks, stems and stem collars, shear blades and butt knockers, die cassettes and horseshoes, bolsters and die rings, pressure rings and plates, cleanout blocks, and alignment barrels. We build up to 96" in length and diameter and up to 100,000 lbs.

+
-

What is a container reline, and why does it matter?

A reline puts a new liner in a worn extrusion container. Liners wear slowly enough that output often slips before anyone notices, and a reline costs a fraction of a new container. We run four relines a week and tune up on-board heating systems while the container is here.

+
-

Should we keep a backup container?

Yes. A backup container with a new or refurbished liner lets you swap containers and keep the press running while the worn one is relined.

+
-

Can you stock dummy blocks for us?

Yes. We stock dummy blocks for 90+ customers, including quick-change designs built for fast rotation. Running out of dummy blocks is the most common reason extruders call us for an emergency shipment.

+
-

How long does a container reline take?

It depends on the container and what we find once it's apart. One recent emergency reline was relined and delivered in 3 days. That's a real example, not a guarantee. We reline four containers a week, so it's easier to fit one into the schedule before the liner fails than after.

+
-

How do you know when an extrusion press stem needs replacing?

Look at the working end. A bell-mouth condition, where the end has flared out, is the wear pattern that tells you the stem is at the end of its service life. Replace it on your schedule, before it lets go mid-shift.

The stem of an aluminum extrusion press being milled.

Wherever You’re Located, We’re Here to Help

17 strategic locations in North America to meet the needs of our diverse customer base.

Get to know us. Get in touch today.

We have the resources to meet any part or production challenge. Let’s talk about what that means for you.

"*" indicates required fields

This field is for validation purposes and should be left unchanged.
Privacy Policy*