TTE, MSCED, TRD

Machining and Heat Treat for Aluminum Extrusion Tooling

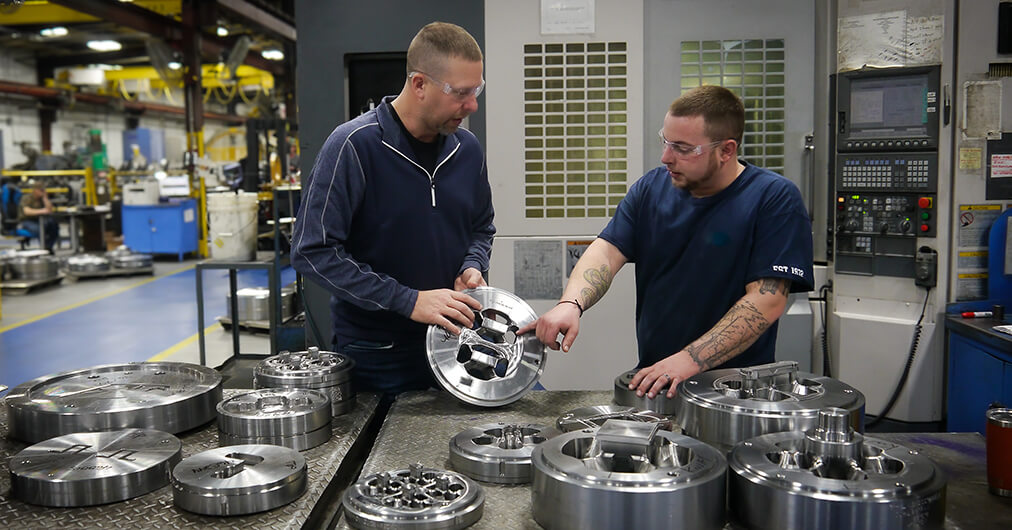
Five U.S. locations, 221,000 sq. ft. of production space, and 155+ mills, lathes, EDMs, and grinders. Michigan and Alabama adds in-house heat treat and nitriding so your tooling stays under one roof.

of production space
221000 sq. ft.
Mills, Lathes, EDMs, & Grinders
155 +
ISO 9001:2015 Certified
ISO 9001
U.S. Locations
5

155+ mills, lathes, EDMs, & grinders, All Dedicated to Extrusion Tooling

The count covers CNC, manual, and EDM equipment across all five locations. CAD/CAM runs networked into the CNC machines, so a die you reorder six months from now is cut to the same geometry as the first one. Paired with our massive in-house heat treat department, we’re able to move your order from design to finished tooling without it leaving our own floor.

  • 5-Axis Mills (6)
  • CNC Mills (59)
  • Boring Mills (4)
  • Manual Mills (15)
  • Lathes (27)
  • Wire EDM (24)
  • Sinker EDM (11)
  • Blanchard (6)
  • Extrude Hones (3)

In-House Heat Treat and Nitriding

We run complete in-house heat and nitriding processes at our Michigan and Alabama locations.

Combined with decades of experience in steel selection, customers trust us to extend extrusion speed and total pounds extruded over the life of their tooling.

We employ two heat treat processes based on the size of the tool:

  • Smaller tooling runs on an automated fluidized bed line.
  • Larger tooling goes through conventional high-heat furnaces.

Both are cooled in temperature-controlled chambers after the initial heat process, then move to draw ovens for tempering.

Nitriding runs on its own equipment and takes tooling from either route.

Equipment & Capabilities FAQ

FAQs
+
-

What equipment do you use to build aluminum extrusion tooling?

155+ mills, lathes, EDMs, and grinders across five U.S. locations. CAD/CAM runs networked into the CNC machines, so a die you reorder six months from now is cut to the same geometry as the first one.

+
-

How are aluminum extrusion dies heat treated?

By size. Smaller tooling runs on an automated fluidized bed line. Larger tooling goes into high-heat box furnaces, then a temperature-controlled room where it cools at the same rate year-round, then draw ovens for tempering. Either way the tool is brought to temperature, quenched, and tempered. The controlled room matters because cooling too fast warps and cracks dies. Before it existed, tools cooled at whatever the shop temperature happened to be that day.

+
-

Where do you heat treat and nitride?

In-house at our Michigan and Alabama locations. Nitriding runs on its own equipment and takes dies from either heat treat route.

Wherever You’re Located, We’re Here to Help

17 strategic locations in North America to meet the needs of our diverse customer base.

Get to know us. Get in touch today.

We have the resources to meet any part or production challenge. Let’s talk about what that means for you.

"*" indicates required fields

This field is for validation purposes and should be left unchanged.
Privacy Policy*